
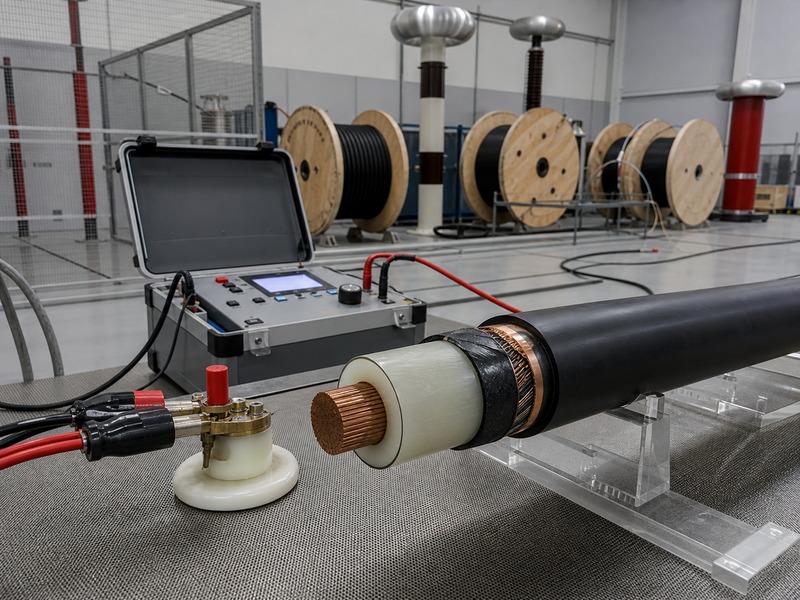
Prije otpreme, XWA Cable potvrđuje da je svaka narudžbina srednjenaponskog kabla završila rutinska ispitivanja koja se zahtijevaju odobrenom tehničkom specifikacijom i da izvještaj o ispitivanju odgovara stvarnoj proizvodnoj seriji. Za IEC 60502-2 kabl, pregled obično pokriva otpor provodnika, djelomično pražnjenje, ispitivanje napona, građevinske mjere, identifikaciju, i dokumentima definisanim ugovorom. Testovi tipa i uzorci služe različitim svrhama i ne treba ih brkati sa rutinskim testovima.
Cilj nije prikupiti debeo paket dokumenata. Cilj je povezati svaki bubanj i test zapise na odobreni dizajn kabla. Izvještaj o testiranju bez šifre kabla, oznaka napona, veličina provodnika, referenca bubnja ili lota, metoda ispitivanja, rezultat, datum, and responsible inspection record provides limited traceability.
This article presents XWA Cable’s factory testing, sljedivost, and document-control perspective for EPC, korisnost, and industrial projects. It explains how XWA organizes test evidence and links it to the supplied cable. The MV Power Cable product page provides the commercial product context; this article focuses on acceptance before shipment.
Start By Separating Routine, Uzorak, And Type Tests
Rutinska ispitivanja primjenjuju se na proizvedene duljine kabela prema standardu i specifikaciji projekta. They help detect production defects in the supplied cable. Sample tests apply to selected samples or completed cable at defined frequencies. Type tests validate a cable design or system under more extensive conditions. Oni ne dokazuju da je svaki novi bubanj prošao svaku proceduru tipskog ispitivanja.
Specifikacije projekta ponekad koriste izraz "svi testovi" bez definiranja kategorije. XWA odvaja rutinu, uzorak, tip, i posebne testove jer odgovaraju na pitanja različitog kvaliteta. Odobreni plan inspekcije navodi koja se rutinska ispitivanja primjenjuju na proizvedene dužine, koja se ispitivanja uzoraka primjenjuju na seriju, i koji dokazi o tipskom ispitivanju podržavaju dizajn kabla.
| Test Category | Primary Purpose | Tipični dokazi | Fabrička kontrolna tačka |
|---|---|---|---|
| Rutinski test | Provjerite proizvedene dužine kabela | Izvještaj o fabrici vezanom za seriju/bubanj | Pod pretpostavkom da generički certifikat pokriva pošiljku |
| Test uzorka | Provjerite odabrane proizvodne uzorke | Izvještaj o uzorku serije i mjerenja | Očekujem da će svaki bubanj dobiti destruktivne provjere |
| Test tipa | Potvrdite dizajn kabla | Certifikat ili izvještaj specifičan za dizajn | Using an unrelated design report |
| Special/project test | Meet contract or utility requirement | Approved inspection and test plan | Adding tests after production without agreement |

The Approved Datasheet Is The Test Report’s Reference Point
Testing starts with document control. Prije proizvodnje, XWA confirms cable designation, nazivni napon, materijal i veličina provodnika, ekran provodnika, XLPE izolacija, izolacioni ekran, metalni ekran, blokiranje vode, oklop, vanjski omotač, standard, dužina bubnja, i obeležavanje. The test report should refer to that approved construction.
If a quotation references 33kV Cable but the final approved specification uses a 18/30(36)kV designation, the documents must stay consistent. If the approved project requirement changes copper screen area, oklop, or sheath after approval, the inspection plan may also change. A report that lists only “MV cable 240 mm2” does not identify the product well enough.
For project selection background, XWA provides the Medium Voltage Cable Selection Guide. The same variables used during selection must appear in production and acceptance records.
Conductor Resistance: A Basic Test With Commercial Consequences
Conductor resistance confirms whether the conductor meets the applicable requirement after correction to the reference temperature. It can reveal problems with conductor material, presjek, konstrukcija pramena, zglobova, or measurement. The report should state the measured value, correction basis, limit, and result.
XWA checks that the report uses the correct conductor material and size. Copper and aluminum limits differ. Conductor class also matters. A result without units or temperature correction cannot be reviewed properly. If the project includes several sizes, each size needs the correct acceptance limit.
Resistance also connects to project performance. A cable can pass resistance requirements and still need a separate project ampacity or voltage-drop study. Factory resistance testing verifies product conformity; it does not replace system design calculations.
Partial Discharge: Important, But Easy To Oversimplify
Partial discharge testing is central to many MV cable acceptance regimes because defects in the insulation system, ekrani, or interfaces can create localized electrical discharges. The test should follow the applicable standard and agreed voltage conditions. XWA does not reduce partial-discharge control to a single phrase such as “PD passed.”
The report should identify the cable, test setup or method reference, ispitni napon, measured level or acceptance statement, background noise control where relevant, and result. The laboratory must use suitable equipment and procedures. Cable ends and test terminations also matter because a poor temporary termination can influence measurements.
A low reported value is not useful if the report cannot be linked to the shipment. I obrnuto, a test anomaly does not automatically prove the entire production lot is defective. The supplier should investigate the setup, prestanak, oprema, and cable before deciding on disposition. XWA records the investigation, disposition, and retest whenever a nonconformity occurs.
Voltage Testing Checks Insulation Integrity Under Defined Conditions
Voltage testing applies a specified test voltage for a specified time under the relevant standard or contract. It checks insulation integrity after manufacturing. The exact method and level depend on the cable rating and governing specification. XWA applies the voltage level and duration defined by the applicable standard and approved project specification.
The report should list the rated voltage designation, ispitni napon, trajanje, test frequency or method, cable length or drum reference, and result. A simple “high voltage test OK” entry lacks enough information for technical review.
Voltage testing does not prove every aspect of long-term cable performance. It works with construction control, material checks, ispitivanje delimičnog pražnjenja, uzorci testova, and type-test evidence. Acceptance depends on the complete quality plan.
Construction Measurements And Visual Inspection
Electrical tests receive attention, but dimensional and visual checks often catch practical configuration deviations. XWA confirms conductor construction, debljina izolacije, screen dimensions, copper wire or tape screen area, oklop, debljina omotača, ukupni prečnik, obeležavanje, and drum length against approved data.
Insulation thickness deserves careful review because MV electric stress depends on the designed insulation system. Screen surfaces and interfaces should be smooth and compatible. Metallic screen construction must match the fault-current and bonding design. Armor must match the installation environment and single-core cable requirements. Outer sheath quality affects moisture protection and handling.
| Inspection Item | What To Match | Common Configuration Error |
|---|---|---|
| Dirigent | Materijal, veličina, klasa, konstrukcija pramena | Wrong material or unclear class |
| Izolacija | Materijal, nominal/minimum thickness, čistoća | Only recording nominal value |
| Metalni ekran | Copper wire/tape design and area | Ignoring earth-fault requirement |
| Oklop | Material and construction | Using unsuitable armor on single-core cable |
| Vanjski omotač | Materijal, debljina, boja, obeležavanje | Missing UV, vatre, or project requirement |
| Drum | Dužina, serial number, ends, pakovanje | Report not linked to drum list |
XWA Pre-Shipment Documentation Package
A practical pre-shipment package should contain the approved datasheet, inspection and test plan, izvještaj o rutinskom testiranju, applicable sample-test report, type-test evidence when required, bubnjeva lista, lista pakovanja, cable marking details, and pre-shipment photos. The contract may require more or less, but the documents should form one traceable set.
The inspection and test plan should define hold points and witness points before production begins. When the project requires witnessed partial-discharge or voltage tests, XWA schedules the hold and witness points before production. A request made after the cable is packed can cause delay, rehandling, or disagreement.
Photos should show cable markings, drum numbers, cable ends, drum condition, zaštita, and container loading when required. Photos are not test evidence, but they help verify identity and packing. The new media metadata process should also describe these images accurately in the WordPress library when they support public content.
Sljedivost: Connect The Cable, Drum, Lot, And Report
Traceability is the difference between a report and useful acceptance evidence. Each manufactured length should connect to a drum number, tip kabla, veličina, proizvodna partija, and test result. The drum list should connect those numbers to shipping documents.
If a project receives fifty drums, XWA’s traceability system shows which tests apply to each length and which sample tests apply to the batch. If a nonconformity affects one lot, the system defines the affected scope without placing the entire shipment under uncertainty.
Factory Acceptance Testing And Third-Party Inspection
Some EPC projects use a factory acceptance test or third-party inspector. This can improve transparency, but only when the scope is clear. An inspector cannot verify an undefined specification. XWA confirms the approved datasheet, plan testiranja, acceptance criteria, document list, and sampling plan before the visit.
The inspector should verify equipment identification and calibration status, cable identity, uslove ispitivanja, results, obeležavanje, drum condition, and document consistency. A short visit cannot replace manufacturing quality control. It checks selected evidence at an agreed stage.
Third-party inspection also does not make an unsuitable cable design suitable. Design approval belongs before production. FAT confirms that the supplied cable and documents match the agreed requirements.
Common Problems In MV Cable Test Reports
- The report lacks drum or lot references.
- The voltage designation differs from the approved contract specification.
- Conductor resistance has no temperature correction or limit.
- Partial discharge is marked “pass” without test conditions.
- Voltage test level or duration is missing.
- The report uses a generic product description.
- Type-test evidence belongs to a different cable construction.
- Područje ekrana, oklop, or sheath requirements are absent from inspection records.
- Calibration status is not available when the contract requests it.
- Drum list and packing list use inconsistent identifiers.
How To Handle A Nonconforming Result
A failed or questionable result needs a controlled response. The supplier should identify the affected cable, stop release, investigate the test setup and production record, define the cause, and propose correction or rejection. Retesting should follow the agreed standard and quality procedure.
XWA issues a nonconformity record that preserves the original result, investigation, disposition, corrective action, retest, and approval. The original result remains part of the quality record. Transparent records build more trust than pretending that production never has deviations.
Testing Does Not End At The Factory Gate
Factory tests cannot protect a cable from poor shipping, storage, povlačenje, savijanje, or termination work. Heavy MV cable drums need suitable packing, chocking, unloading, storage, and end sealing. Installation teams must respect bending radius, povlačenjem napetosti, and sheath protection.
After installation, project specifications may require sheath tests, insulation checks, VLF or other commissioning tests, or accessory tests. These are separate from factory routine tests. The owner, consultant, dobavljač kablova, and accessory supplier should agree on the commissioning method.
Project Data XWA Confirms Before Production
- Cable voltage designation and system voltage.
- Materijal provodnika, veličina, and class.
- Izolacija, ekrani, metalna površina ekrana, oklop, i omotač.
- Applicable standard and project deviations.
- Required routine, uzorak, tip, and special tests.
- Inspection and test plan with hold/witness points.
- Required report format and traceability fields.
- Third-party inspection scope, if any.
- Dužina bubnja, drum numbering, pakovanje, and photos.
- Destination port, shipping term, and project schedule.
FAQ
Does every MV cable drum need partial discharge testing?
The applicable standard and approved project specification determine the routine test scope. XWA applies the requirement defined by the standard and project specification, and the report identifies the manufactured cable length.
Is a type-test certificate enough for shipment acceptance?
br. Type-test evidence validates a design under defined conditions. Shipment acceptance also needs current routine and sample-test evidence, sljedivost, construction checks, i ugovornu dokumentaciju.
What should an MV cable routine test report include?
It should identify the cable, veličina, napon, standard, lot or drum, metoda ispitivanja, conditions, measured result, acceptance limit, datum, equipment or procedure reference, and approval.
Can EPC Project Teams Witness Factory Tests?
Witnessing can help on critical projects, but the scope and hold points must be agreed before production. Clear documents and traceability remain necessary even when an inspector attends.
Can factory tests guarantee installation performance?
br. Factory tests confirm manufacturing conformity under defined conditions. Shipping, storage, povlačenje, savijanje, spajanje, prestanak, and commissioning still affect project performance.
XWA Factory Quality View
Ispitivanje SN kabla prije otpreme trebalo bi stvoriti sljedivu vezu između odobrenog dizajna, proizvedeni kabl, rezultati testa, bubnjevi, i otpremne dokumente. XWA odvaja rutinu, uzorak, tip, i projektne testove umjesto predstavljanja generičkog “testnog certifikata”.
Za tehničku konfiguraciju i ponudu, XWA zahtijeva oznaku napona, veličina provodnika, izgradnja, oblast ekrana, oklop, omotač, standard, količina, dužina bubnja, potrebni testovi, tačke svedoka, dokumenata, i odredišnu luku. XWA Cable može pripremiti tehnički i testni opseg za pregled prije proizvodnje.